DINIS GLOBAL
Quality & Safety

How DINIS treats safety
Safety is treated as a design input rather than a compliance afterthought. It starts in specification, where load cases, restraint and control requirements are defined, and continues through manufacturing, factory testing, installation, commissioning and operator training.
The objective is an attraction that stays inside its designed operating envelope for its whole service life, and that can be inspected, maintained and evacuated by a normally trained local team.
That design-first approach shows up in the field as predictable behaviour: a ride that stays inside its operating envelope, that can be inspected and evacuated by a normally trained team, and that does not surprise the operator at the annual inspection.
In practice, the right answer follows from the site and the standard, not from a catalogue entry. This is the kind of detail that separates a documented delivery from one that is discovered on site.
When comparing suppliers, the page keeps this explicit because it is the step where projects most often drift. The guidance is kept concrete so a buyer can act on it before the first call.
For the operating team, the guidance is kept concrete so a buyer can act on it before the first call. The page keeps this explicit because it is the step where projects most often drift.
Standards and certification approach

DINIS provides CE compliance documentation for applicable models. The exact document set is matched to the delivered configuration and the destination market, because certification scope, inspection route and document language vary by territory.
Rather than asserting compliance broadly, DINIS asks which standard the local authority will accept, then prepares the traceability, test records and manuals to match. Buyers should request the same evidence from every supplier they compare.
The destination standard is the one that matters, which is why DINIS asks which standard the local authority will accept before preparing anything. That question, asked early, avoids the most expensive kind of rework in this industry.
Put simply, the page keeps this explicit because it is the step where projects most often drift. It is matched to the destination standards and the delivered scope before the order is fixed.
Operationally, it is matched to the destination standards and the delivered scope before the order is fixed. The same check should be applied to every supplier a buyer compares.
For project planning, the same check should be applied to every supplier a buyer compares. It is matched to the destination standards and the delivered scope before the order is fixed.
Factory testing and quality control
Manufacturing quality is controlled through material traceability, weld and structural inspection, factory test records and pre-shipment checks. Critical components are verified against the approved drawings before dispatch, and the results travel with the documentation pack.
Each project package defines what is tested, how it is recorded and what the operator receives at handover, so quality is visible in documents rather than asserted in marketing language.
The point of factory testing is continuity: the same data that released the machine from the factory travels with it to the site, so installation and commissioning work from a single verified record rather than from memory or assumption.
For the operating team, the guidance is kept concrete so a buyer can act on it before the first call. The page keeps this explicit because it is the step where projects most often drift.
At the procurement stage, the same check should be applied to every supplier a buyer compares. The guidance is kept concrete so a buyer can act on it before the first call.
In practice, the key is to write this down as a step the site team can execute, rather than leave it as a general intention. The plan only becomes reliable once this item has an owner and a lead time.
Installation, commissioning and acceptance

Installation is defined before shipment so the civil and electrical interfaces are clear. Commissioning includes function checks, safety-device verification and a trial-operation period, with the scope stating which civil works and local approvals remain the buyer’s responsibility.
Acceptance ends with documented checks rather than a signature alone. The operator receives start-up and shutdown routines, inspection points and a spare-parts starting list before opening day.
Commissioning and acceptance are documented because safety claims that cannot be inspected are not worth much. The operator leaves handover with verified checks, routines and a parts list, which is what makes opening day safe and repeatable.
For project planning, the page keeps this explicit because it is the step where projects most often drift. The key is to write this down as a step the site team can execute, rather than leave it as a general intention.
On site, the guidance is kept concrete so a buyer can act on it before the first call. This is the kind of detail that separates a documented delivery from one that is discovered on site.
Put simply, the same check should be applied to every supplier a buyer compares. Getting this right early protects the opening date and the budget.
Operator training and emergency readiness
Operator training covers daily start-up and shutdown checks, restraint or supervision procedures, emergency stop and evacuation practice, and first-line maintenance and inspection access. The goal is a team that can run the ride safely without the supplier on site.
Training is matched to the ride and the destination, and the manuals are prepared in the language agreed during scoping, so the operating team is not working from instructions it cannot read.
Emergency readiness is part of normal operation, not a special case. Start-up, shutdown, restraint and evacuation practice are trained before opening, and the manuals are prepared in a language the operating team can actually read.
Operationally, the guidance is kept concrete so a buyer can act on it before the first call. The plan only becomes reliable once this item has an owner and a lead time.
Put simply, the page keeps this explicit because it is the step where projects most often drift. It is matched to the destination standards and the delivered scope before the order is fixed.
On site, the guidance is kept concrete so a buyer can act on it before the first call. This is the kind of detail that separates a documented delivery from one that is discovered on site.
Inspection, maintenance and documentation over time
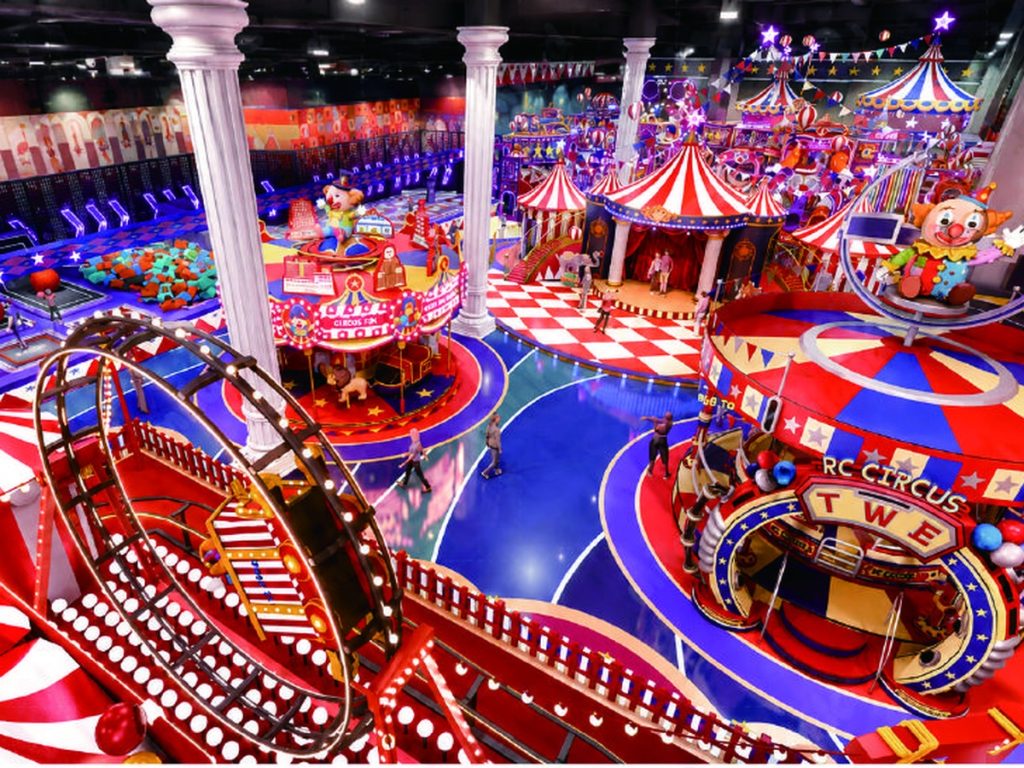
Safety does not end at handover. A documented inspection routine, accessible wear parts and a realistic refresh plan for theming and electrics keep the ride inside its operating envelope across its design life.
DINIS supports that with maintenance schedules, a starting spare-parts list and guidance on which parts to hold locally versus reorder on demand, so an annual inspection does not become an unplanned closure.
Over the asset’s life, safety is maintained through routine: dated inspections, accessible wear parts and a refresh plan that keeps theming and electrics inside their design limits. That routine is cheaper than reactive repair and long closures.
Qualified brief first
When comparing suppliers, the page keeps this explicit because it is the step where projects most often drift. The guidance is kept concrete so a buyer can act on it before the first call.
In practice, it is matched to the destination standards and the delivered scope before the order is fixed. DINIS treats this as a verification step, and the evidence is checked before anything is committed.
At the procurement stage, this is the kind of detail that separates a documented delivery from one that is discovered on site. The right answer follows from the site and the standard, not from a catalogue entry.